

2026-11-20
Key Factors in Selecting a High Speed Board to Board Connector for BMS
View More

 FPC/FFC Connector
Board to Board Connector
Wire to Board Connector
Flexible Flat Cable
RF Connector
I/O Header
Product
Automotive
Product
 141091-211260
 Consult

Electric vehicles rely on multiple electronic systems to coordinate power conversion, battery operation, vehicle control, and driver assistance. Behind these functions are numerous printed circuit boards (PCBs) that process signals, manage power, and communicate with other modules.
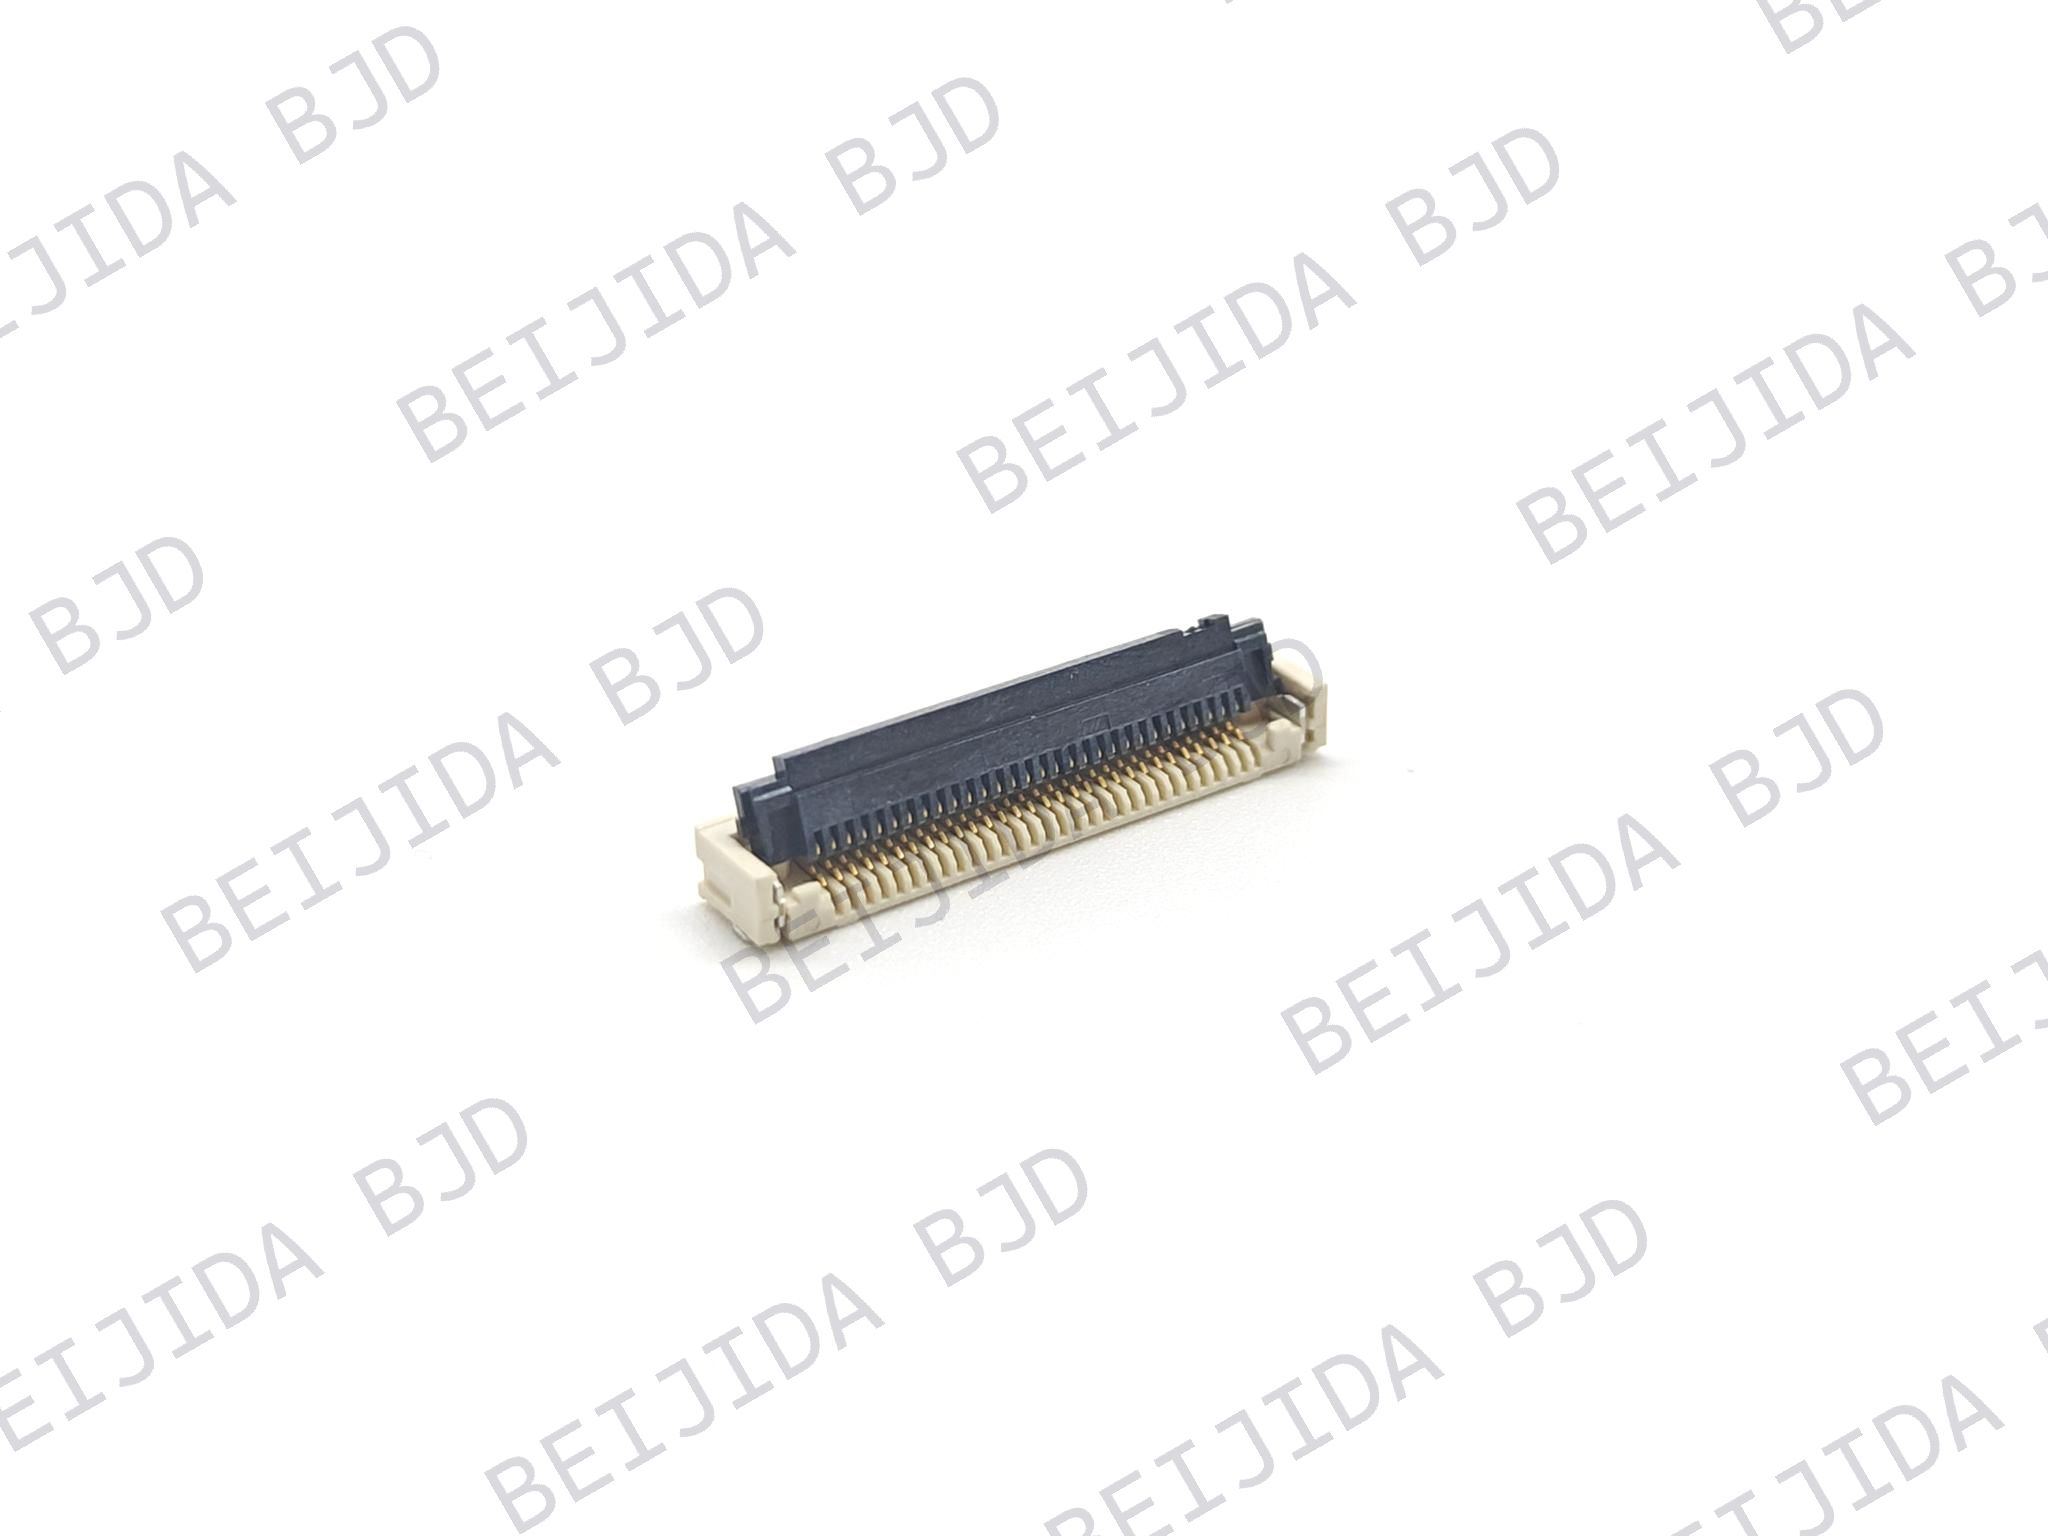
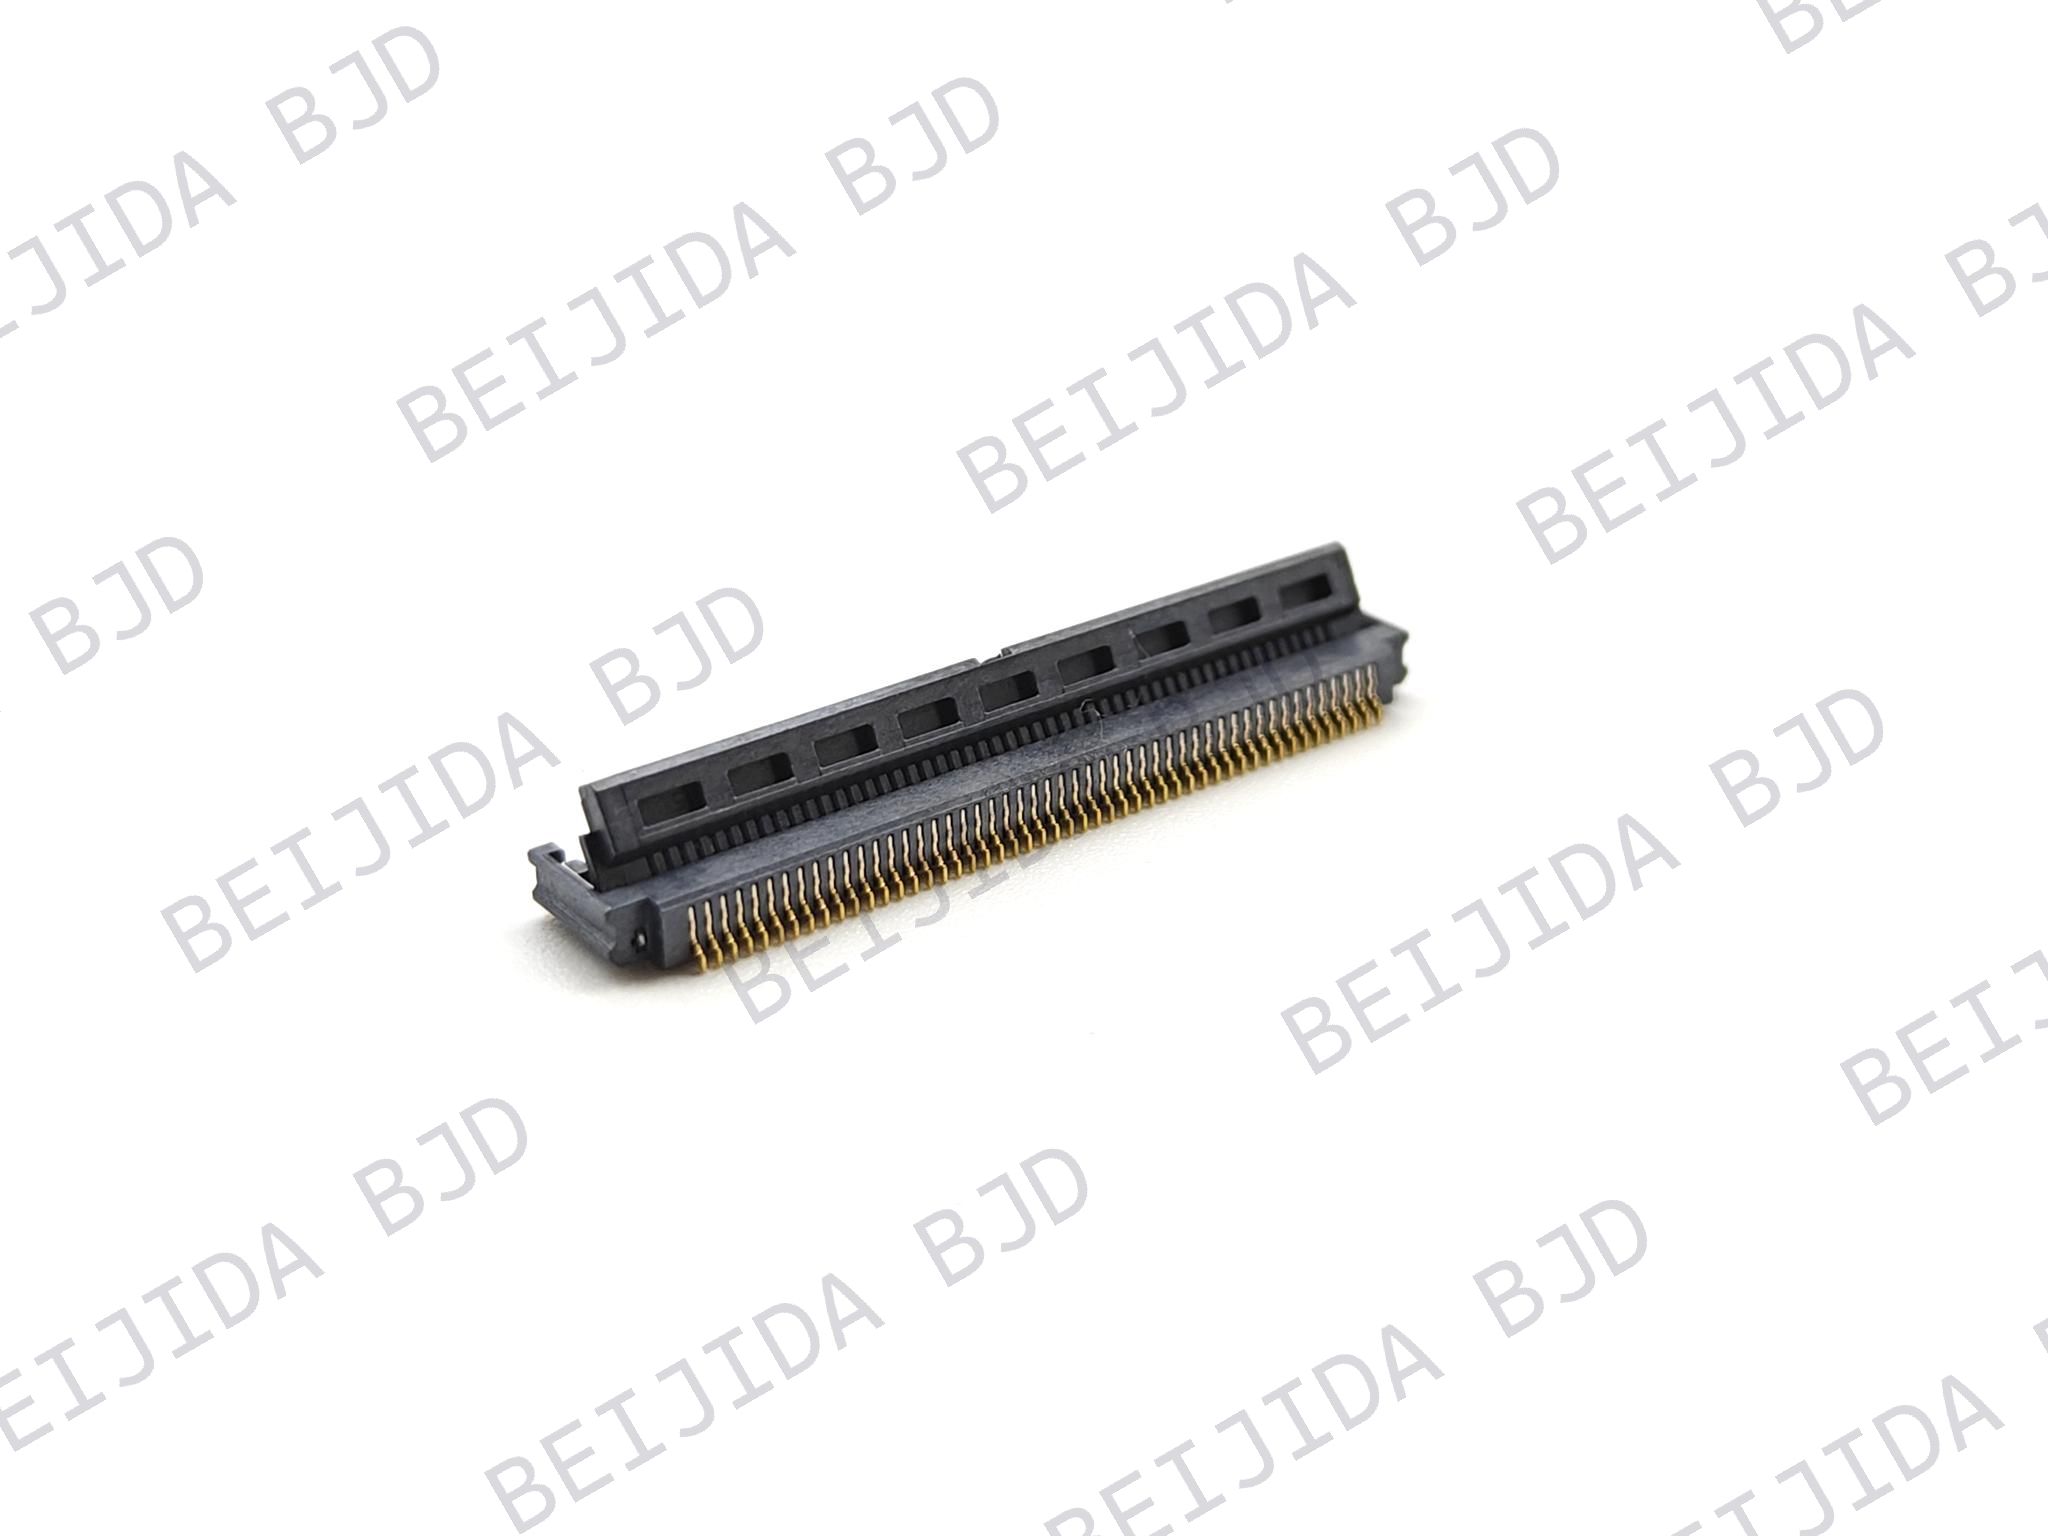
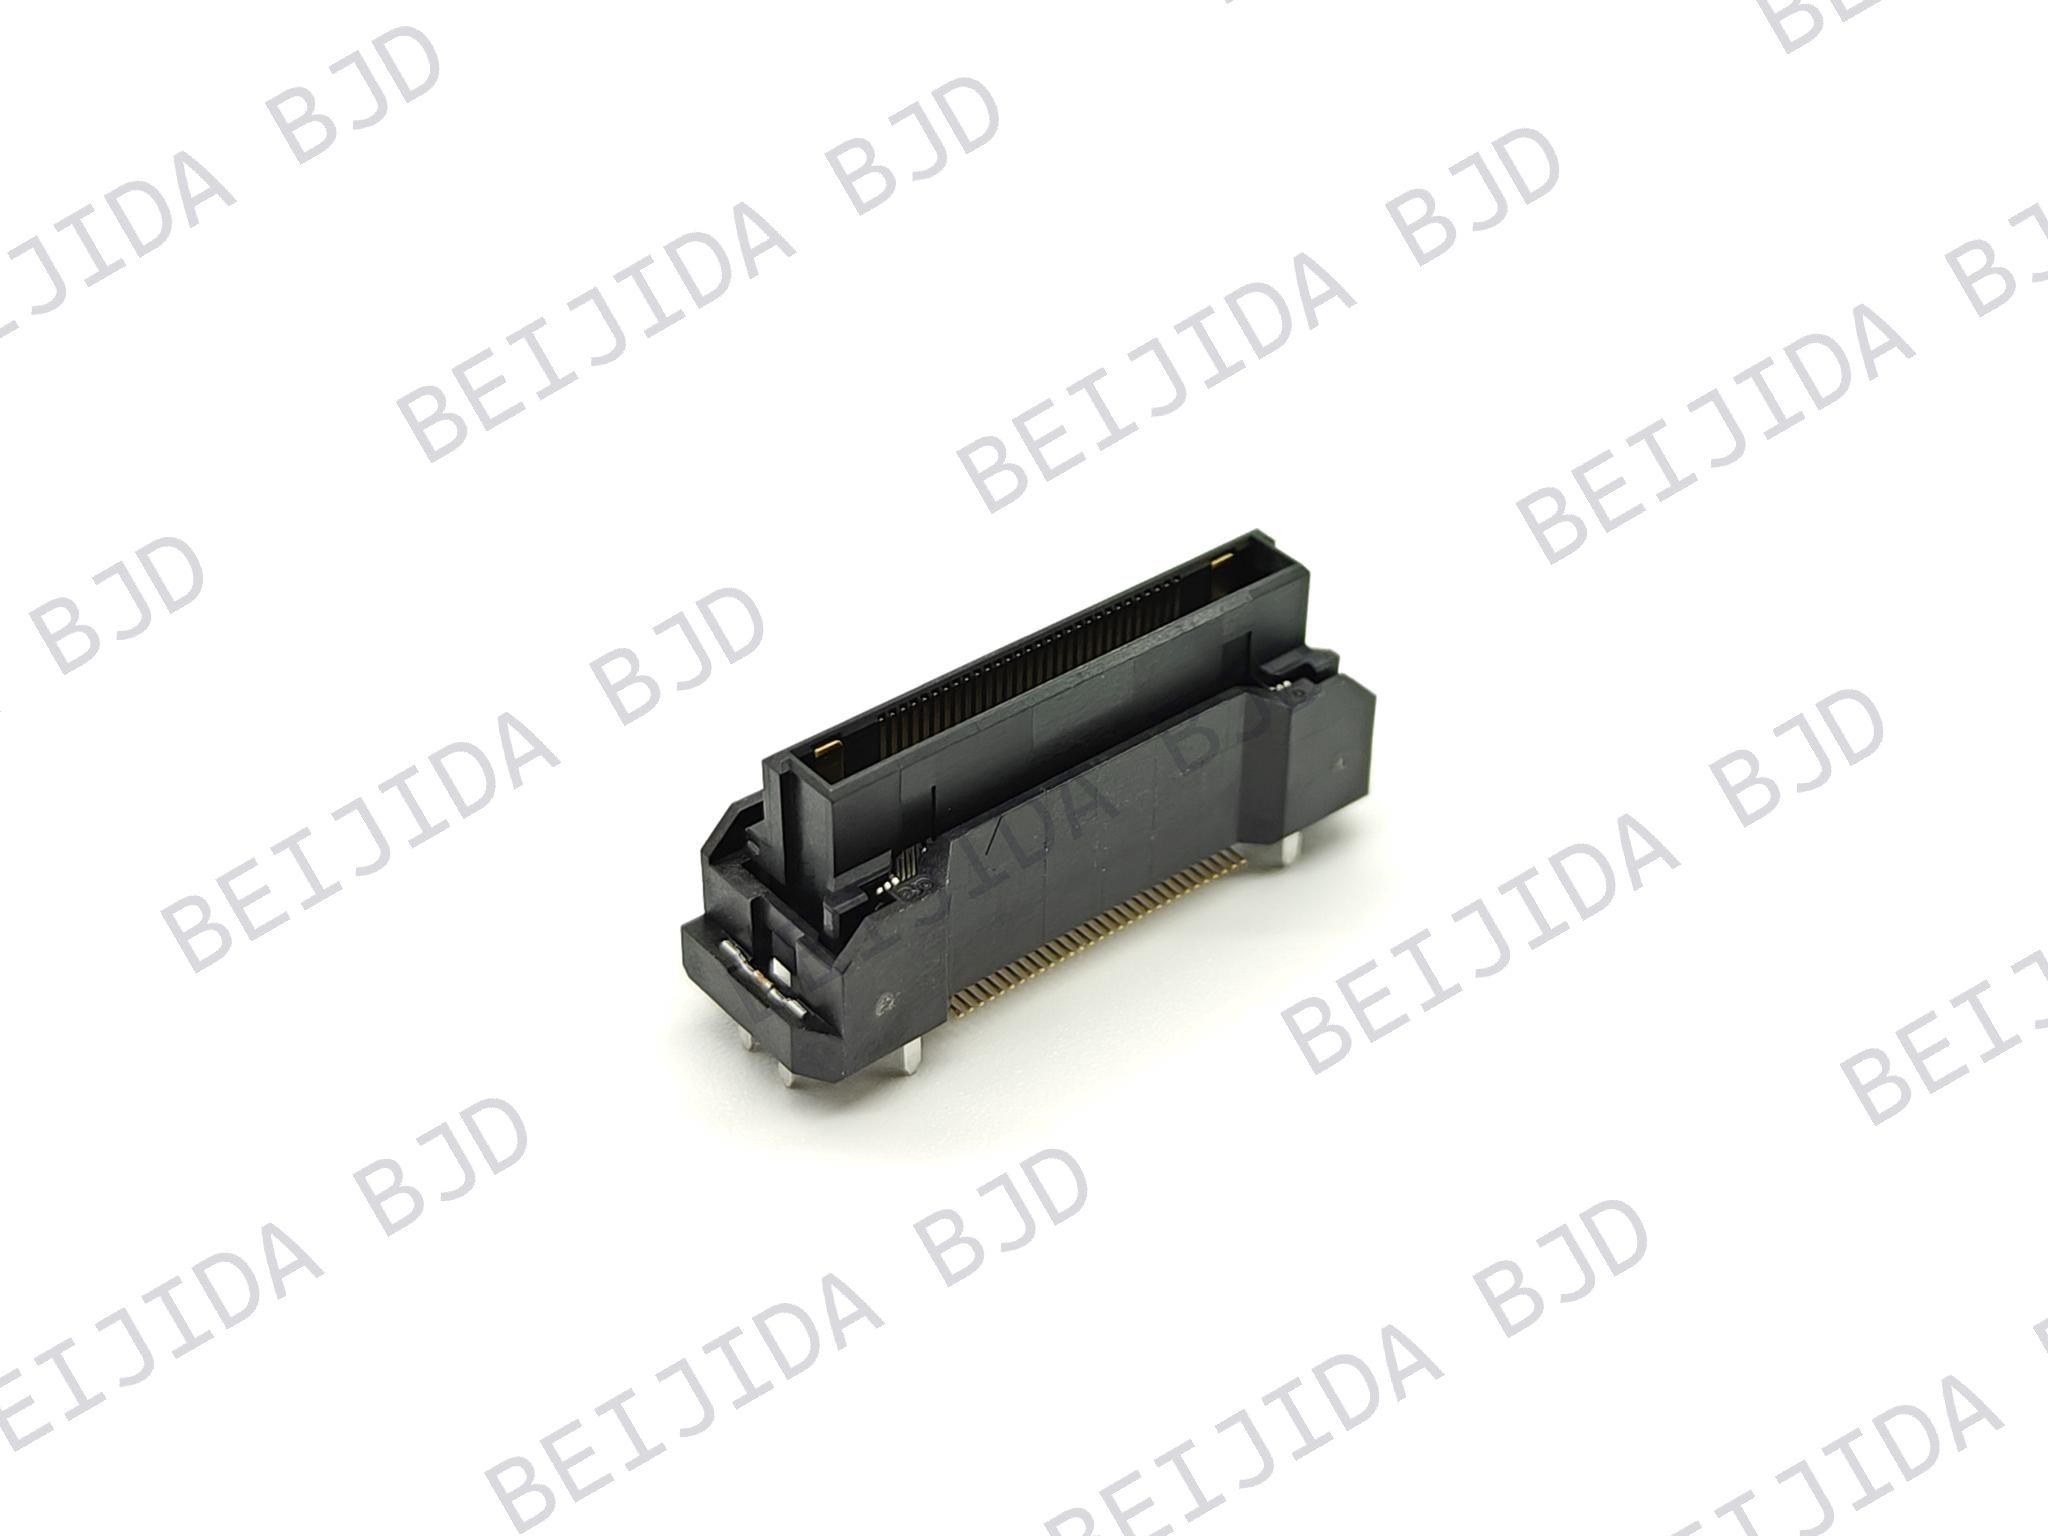
A board to board connector for EV applications provides a direct electrical interface between separate PCBs. Beyond establishing contact, it influences module dimensions, board arrangement, electrical routing, and assembly methods. As EV architectures become more integrated, engineers need to understand how these connections fit into the complete electronic system.
Different EV subsystems have different control and communication requirements. Some use separate PCBs to divide processing, power management, and interface functions. Board to board connectors can provide direct electrical links between these boards without requiring additional cable assemblies.
Several electronic areas are worth considering.
A battery management system monitors battery conditions and supports functions such as voltage measurement, temperature monitoring, protection, and control. Depending on its architecture, the BMS may contain a main control board and additional monitoring or interface boards.
Board to board connectors can be considered for internal connections between these PCBs when the electrical and mechanical requirements are suitable. Typical connection functions may include:
Low-voltage battery monitoring signals
Temperature sensing and control signals
Communication between monitoring and control boards
Specified low-voltage power connections within the electronics
These connections should not be confused with the battery's main power path. A conventional signal-level board to board connector is not a substitute for a high-voltage battery power connector. Its rated current, voltage, insulation design, and contact configuration must match the actual circuit.
The electric powertrain involves electronic functions such as motor control, power conversion, and system monitoring. These functions may be distributed across different circuit boards within a control unit.
A board to board connection can link processing and interface boards where the design uses a multi-board arrangement. The required configuration depends on whether the connection carries control signals, communication data, or a specified power load.
Engineers should also consider the physical arrangement of these boards:
Vertical connections can support stacked PCB configurations.
Right-angle connections can accommodate boards positioned at approximately 90 degrees.
The connector's height and mating direction must fit the enclosure and surrounding components.
EVs also contain electronic modules for lighting, seating, body functions, and other auxiliary systems. These applications may use multiple PCBs to separate control logic, input and output interfaces, and supporting circuits.
In these designs, board to board connectors can simplify internal interconnection and reduce the need for separate wiring between closely positioned boards. Selection should reflect the module's pin count, electrical load, mounting direction, and available assembly space.
The value of a board to board connector becomes clearer when we look at how electronic modules are organized. Its function extends beyond electrical contact to the physical relationship between PCBs.
Separating electronic functions across multiple boards can make a module easier to organize. A control board may handle processing, while another manages external interfaces or supporting circuits.
A direct board to board connection allows these sections to communicate within the same assembly. It can also help establish a repeatable mechanical relationship between the boards.
However, dividing a circuit across several PCBs introduces additional design considerations:
Contact arrangement and pin assignment
Board spacing and connector height
Signal routing between the connected boards
Mechanical support and assembly access
The connection should be planned as part of the circuit architecture rather than added after the PCB layout is complete.
The relative positions of two PCBs determine which connector orientation is appropriate.
Parallel mating: The two boards remain parallel, commonly in a stacked arrangement. The connector establishes a defined mated height between them.
Right-angle mating: The boards are positioned at approximately 90 degrees, supporting a different three-dimensional layout.
Coplanar mating: The boards occupy the same plane and connect along the board surface.
Each arrangement creates different requirements for connector height, available clearance, mating direction, and mechanical support.
For EV modules with restricted enclosure dimensions, selecting the connection orientation early can help avoid conflicts with nearby components, shielding structures, and mounting features.
Reducing module size is not simply a matter of choosing a smaller connector. Engineers must also consider the space required for mating, inspection, and manufacturing.
A fine-pitch connector may accommodate more contacts within a limited footprint, but the PCB layout still needs sufficient clearance around the connector. The assembly process also requires access to the mating area.
The final design should balance:
Contact density and pin count
Connector height and board spacing
Clearance around nearby components
Assembly and inspection requirements
This approach helps prevent a compact connector choice from creating unnecessary manufacturing difficulties.
Not every board to board connection in an EV carries the same electrical load. A monitoring interface, communication link, and power distribution connection can require very different contact configurations.
For signal connections, engineers should review the number of required contacts, contact resistance, voltage rating, and signal transmission requirements.
Power connections require additional attention to current capacity and temperature rise. A connector with dedicated power contacts may be more suitable when a design needs both signal and power connections in one interface.
BJD's 0.8-12 Series, for instance, provides separate signal and power contact configurations. Its published specifications include:
Signal contact rated current: 0.5 A
Power contact rated current: 5 A
Signal contacts: 40 or 120 pins
Power contacts: 4 pins
These values apply to the specified configuration and should not be generalized to every board to board connector. The contact groups must be matched with their intended circuit functions and actual electrical loading conditions.
Some EV electronic modules exchange data between processing and interface boards. When high-speed signals pass through a board to board connector, connector performance becomes part of the overall transmission channel.
The evaluation should include more than a headline transmission rate. Engineers need to consider:
Impedance continuity
Signal routing and grounding
Crosstalk and insertion loss
PCB layout on both sides of the connection
The connector, PCB traces, and surrounding structures work together as one electrical path. A suitable connector specification therefore needs to be evaluated within the actual design rather than in isolation.
Different EV modules can experience different temperature conditions depending on their location, heat sources, and cooling arrangements.
A connector installed near a power electronic component may face a different thermal environment from one located in a passenger-compartment control module. Engineers should identify the expected operating temperature at the connector itself and compare it with the product's specified operating range.
Temperature also affects contact performance and material behavior over time. The connector's rating should therefore be considered alongside the module's thermal design and validation requirements.
Electrical specifications alone cannot determine whether a connector is suitable. The mechanical interface must also remain compatible with the PCB structure throughout assembly and operation.
Mated height determines the distance maintained between two connected PCBs. It influences overall module thickness and the space available for components between or around the boards.
Contact pitch and pin count determine the connector's physical footprint and connection density. A smaller pitch may help save PCB area, while a larger pitch may suit designs requiring a different contact arrangement or mechanical configuration.
These parameters should be evaluated together. Selecting a connector based only on pitch can lead to an unsuitable mated height or incompatible PCB footprint.
When two PCBs are assembled, their actual positions may differ slightly from their nominal design positions. Component placement variation, board dimensions, housing tolerances, and assembly conditions can all contribute to alignment differences.
A floating board to board connector can accommodate a defined amount of positional deviation between mating boards. This can be useful when the mechanical structure does not allow perfect alignment.
When evaluating a floating connector, engineers should check:
The available movement in the X, Y, and Z directions
The calculated tolerance stack-up of the complete assembly
The board positioning and mechanical support structure
Whether the floating range is sufficient for the actual mating conditions
Floating capability does not eliminate the need for proper PCB positioning. It should be selected according to the actual assembly tolerances.
BJD offers floating board to board connector configurations with different compensation ranges. The appropriate option depends on the required movement direction, board arrangement, and electrical specifications.
Many board to board connectors use surface-mount technology (SMT), allowing them to be assembled with other PCB components through automated production processes.
Before finalizing a design, engineers should check the following:
Recommended PCB land pattern and pad dimensions
Soldering conditions and component placement
Connector coplanarity requirements
Mating height and contact arrangement
Plug and receptacle compatibility
Prototype assembly and inspection can help identify incomplete mating, misalignment, or solder-joint defects before the design moves into volume production.
At BJD, we provide board to board connector options for different PCB structures and electrical requirements. Our product range includes multiple pitches, pin counts, mated heights, connection orientations, and floating configurations.
These variations allow engineers to evaluate connector structures according to the function and layout of each EV electronic module.
For compact PCB assemblies, our 0.4 mm Floating Board-to-Board Series features:
0.4 mm pitch
3 mm mated height
XY floating tolerance of ±0.4 mm
20, 30, 40, 50, and 60 contacts
Operating temperature range of -40°C to +125°C
For applications requiring a different combination of signal and power contacts, our 0.8-12 Series provides 0.8 mm pitch configurations with separate signal and power contact groups. This structure can be considered when the PCB interface needs to accommodate both types of connections.
We also offer the B3501 Series for applications with higher current requirements. Its published configuration includes:
Two contacts
3.5 mm pitch
30 A rated current
X/Y/Z floating tolerance of ±1.0 mm
Its electrical and mechanical specifications make it a distinct option from fine-pitch signal connectors. However, suitability must still be confirmed against the intended circuit and installation conditions.
You can explore our board to board connector product range to compare available configurations. We recommend reviewing the mating pair and complete technical specifications before selecting a connector for a specific EV project.
For EV projects, connector selection often involves coordination between electrical design, mechanical engineering, PCB layout, and manufacturing teams. A connector supplier should therefore provide more than a product catalog.
At BJD, we support connector evaluation by reviewing key design information, including:
Pitch, pin count, and mated height
Connection orientation and floating range
Current and voltage requirements
PCB footprint and mating conditions
Operating temperature and environmental requirements
Our manufacturing capabilities cover processes including stamping, injection molding, and automated production. We also maintain quality management systems including IATF 16949, ISO 9001, and ISO 14001, together with a CNAS-accredited laboratory.
For an EV application, the final validation plan should reflect the actual module environment. Depending on the project, this may include temperature cycling, vibration exposure, contact resistance monitoring, current loading, and inspection of solder joints after environmental testing.
We encourage customers to confirm connector specifications against PCB drawings, mating conditions, and operating requirements. Sample evaluation is an important step before approving the final design for production.
Board to board connectors support the internal interconnection of EV electronic systems, from battery management and powertrain control electronics to body and auxiliary modules. Their role depends on the function of the connected boards, the electrical signals involved, and the mechanical arrangement of the assembly.
At BJD, we offer different board to board connector configurations to support a range of electronic design requirements. By evaluating the complete PCB interface and validating the selected mating pair, engineers can develop a more reliable interconnection solution for EV electronic systems.